
Industrial liquid handling requires equipment that offers safety, control, and reliability. A Solvent Barrel Pump helps transfer solvents and other liquids from drums with less manual effort. It also supports cleaner and more controlled dispensing.
Solvents often have special handling requirements. Therefore, the right pump can reduce spills and improve workplace efficiency. It can also make repeated drum-to-container transfers easier.
Industries use these pumps in chemical processing, manufacturing, laboratories, coatings, and maintenance operations. However, selecting the right model requires attention to the liquid, drum size, flow needs, and operating conditions.
For businesses looking for reliable pumping equipment, Malhar Pump provides solutions designed for practical industrial applications.
What Is a Solvent Barrel Pump?
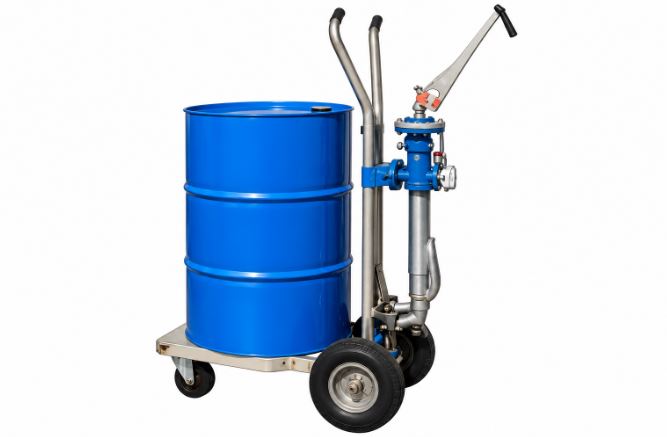
A Solvent Barrel Pump is designed to transfer liquids from drums, barrels, and similar containers. Operators can use it to move liquids into smaller containers or processing systems.
The pump draws liquid from the barrel through a suitable suction tube. It then delivers the liquid through an outlet for controlled dispensing.
These pumps can support different operating methods. Depending on the application, users may choose manual, pneumatic, or other suitable pump designs.
A suitable pump should match the liquid properties. It should also handle the required flow rate and operating environment.
Common Industrial Applications
A Solvent Barrel Pump can support many routine tasks, including:
- Transferring solvents from storage drums
- Dispensing cleaning chemicals
- Moving industrial liquids between containers
- Handling compatible chemical solutions
- Supplying liquids to production equipment
- Supporting maintenance and workshop operations
Therefore, industries can reduce manual handling while improving liquid transfer control.
Why Use a Solvent Barrel Pump?
Manual liquid transfer can create unnecessary handling risks. It may also take more time, especially when workers transfer liquids frequently.
A Solvent Barrel Pump provides a practical way to improve this process. It allows operators to transfer liquids with better control and less physical effort.
One important benefit is controlled dispensing. Operators can manage the transfer according to the application.
Another benefit is convenience. Workers do not need to lift or tilt heavy drums repeatedly.
Furthermore, the right pump can help reduce product waste. Better control can limit unnecessary spills during routine transfer operations.
Key Benefits
A properly selected pump can offer several advantages:
- Easier liquid transfer
- Better dispensing control
- Reduced manual handling
- Improved workplace efficiency
- Lower risk of accidental spills
- Convenient drum-level operation
- Compatibility with selected industrial liquids
However, performance depends on correct pump selection. The pump material must also suit the liquid being handled.
How to Choose the Right Solvent Barrel Pump
Choosing a Solvent Barrel Pump requires more than checking the drum size. The liquid itself plays an important role.
First, identify the chemical properties of the solvent. Check its compatibility with the pump’s wetted materials.
Next, consider the required flow rate. Some applications need controlled dispensing, while others require faster liquid transfer.
You should also check the drum opening and suction tube dimensions. Proper fitting helps create a more practical installation.
Temperature is another important factor. Some liquids require equipment that can operate safely under specific temperature conditions.
Important Selection Factors
Before purchasing, consider these factors:
- Type of solvent or liquid
- Chemical compatibility
- Drum capacity
- Required flow rate
- Pumping method
- Operating temperature
- Suction tube length
- Outlet connection
- Workplace environment
- Maintenance requirements
Additionally, consider how frequently the pump will operate. Regular industrial use may require a more durable construction.
Safe Handling Practices for Solvent Transfer
Using the correct pump is only one part of safe liquid handling. Workers should also follow proper operating procedures.
Before use, inspect the pump and connections. Look for visible damage, leaks, or loose fittings.
Next, confirm that the pump suits the solvent. Never assume that one pump works with every chemical.
Keep the transfer area clean and well organized. Also, avoid unnecessary sources of ignition when handling flammable solvents.
Operators should use suitable personal protective equipment. The required protection depends on the solvent and workplace safety guidelines.
After transferring the liquid, close the container properly. Clean the equipment according to the manufacturer’s instructions.
Maintenance Tips
Regular maintenance can support consistent pump performance.
Inspect seals, tubes, fittings, and other working components regularly. Replace damaged parts before they affect operation.
Also, clean compatible components after use when required. This can help prevent contamination and buildup.
Store the pump in a suitable location when it is not in use. Following the manufacturer’s maintenance recommendations can further improve service life.
Solvent Barrel Pump for Different Industries
Different industries have different liquid handling requirements. Therefore, pump selection should match the application.
Chemical manufacturers may use pumps for controlled solvent transfer. Paint and coating businesses may need equipment for compatible liquids and production materials.
Workshops can use barrel pumps for transferring cleaning fluids. Laboratories may also require controlled dispensing for selected chemical solutions.
Meanwhile, manufacturing facilities often need reliable equipment for repeated material handling.
For these applications, the focus should remain on compatibility, safety, efficiency, and ease of use.
Why Proper Equipment Matters
The wrong pump can create operational problems. It may cause leaks, poor flow, material damage, or unnecessary maintenance.
On the other hand, a properly matched pump can make routine liquid transfer simpler. It can also support a more organized workplace process.
Therefore, businesses should review their application requirements before selecting equipment.
Frequently Asked Questions
1. What is a Solvent Barrel Pump used for?
A Solvent Barrel Pump transfers compatible liquids from drums or barrels. It supports controlled dispensing and reduces manual handling.
2. Can a barrel pump handle every solvent?
No. Pump compatibility depends on the solvent’s chemical properties. Always check material compatibility before use.
3. What factors should I check before buying one?
Consider solvent type, flow rate, drum size, temperature, materials, connections, and operating conditions.
4. Does a barrel pump reduce liquid wastage?
It can improve dispensing control and help reduce spills. However, results depend on correct operation and suitable equipment.
5. How often should a barrel pump be maintained?
Inspection should follow the manufacturer’s recommendations and workplace conditions. Frequent-use equipment may require more regular checks.
Conclusion
A Solvent Barrel Pump can make industrial liquid transfer more controlled, convenient, and efficient. It reduces manual handling and supports practical dispensing from drums.
However, proper selection remains essential. Chemical compatibility, flow requirements, drum dimensions, temperature, and operating conditions should guide the decision.
Businesses should also follow safe handling and regular maintenance practices. For reliable industrial pumping requirements, explore suitable solutions from Malhar Pump and select equipment that matches your specific application.